What should buyers verify before releasing a new hydraulic injection molding machine for shipment?
Define the FAT protocol and request evidence for machine identity, ordered configuration, clamp movement, injection and plasticizing response, hydraulic stability, safety functions, alarm status, trial basis, documents and open items. Keep selected GEERPOWER model, FAT result, sample approval, price, delivery and site commissioning as NEEDS_EVIDENCE until documented for the exact project.
Decision checklist
- Define the FAT protocol before the test starts.
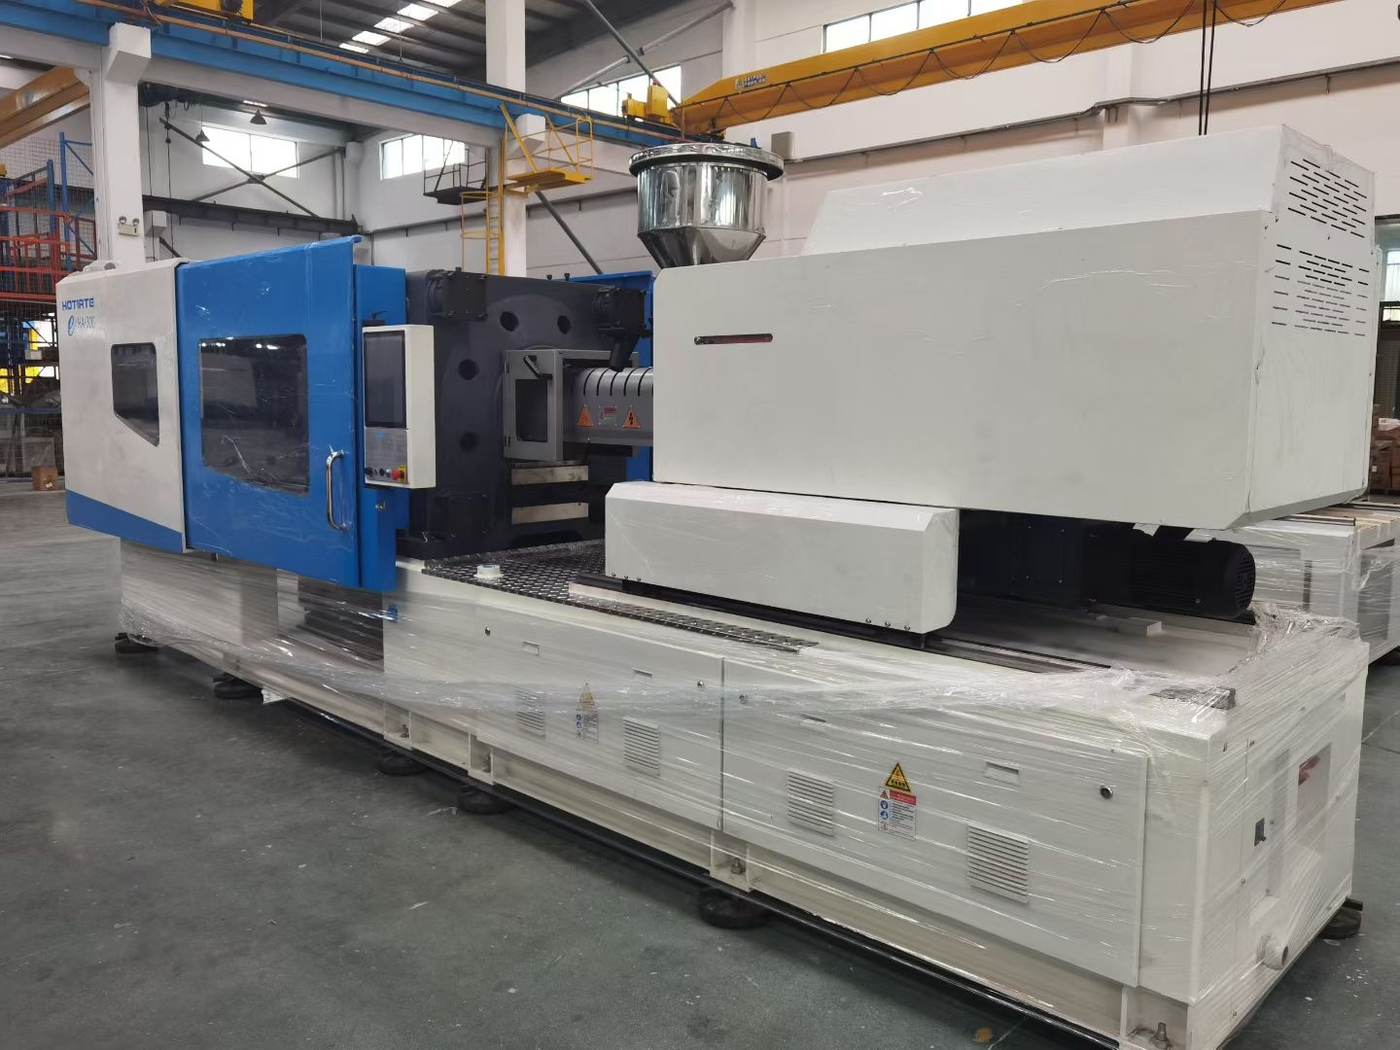
- Confirm nameplate, serial number, controller version and ordered configuration before relying on video evidence.
- Separate no-load movement, mold trial and production acceptance.
- Record safety-function checks and open items before approving packing or shipment.
Ready to ship needs written evidence
A hydraulic injection molding machine should not be released for export only because assembly is complete. For an overseas GEERPOWER project, the buyer should ask what the factory acceptance test will prove and what remains outside the test.
The FAT file should connect the tested machine to the order: nameplate, serial number, controller version, options, hydraulic configuration, safety functions, trial condition, handover package and open-point list. Without that baseline, later shipment, installation or site-utility issues become much harder to separate.
Treat FAT as a shipment decision record, not as a broad promise of site production performance.
Use a FAT evidence table
A simple table keeps the approval decision practical. Mark each line as confirmed, open, excluded or waiting on buyer data instead of turning missing evidence into a pass.
This is especially important when the buyer's mold, resin or destination utilities are not yet available for the factory test. A dry run can verify movement and basic controls; it cannot prove final production quality by itself.
- Machine identity: nameplate photo, serial number, controller version and ordered configuration list.
- Clamp and ejector: open-close movement, mold-height movement, ejector stroke and interlock behavior.
- Injection unit: heater stabilization, screw rotation, injection stroke, pressure-hold response and alarms.
- Hydraulic system: warm-run temperature trend, pressure response, visible leakage and abnormal noise.
- Safety and handover: guards, emergency stop, safety-door interlocks, documents, backups and open points.
Keep FAT and SAT separate
ISO 20430 defines safety requirements for injection moulding machines with hydraulic and/or electrical platen drives, and EUROMAP lists recommendations for injection molding machine testing, interfaces and production data. Those references support a structured FAT discussion, but they do not prove a GEERPOWER project result.
A manufacturer-side FAT is performed under factory conditions before shipment. Site acceptance depends on the buyer's power, cooling water, floor, mold, resin, operators, auxiliaries and peripheral interfaces. Any site output, cycle, dimensional or commissioning claim should remain evidence-gated until the site test records exist.
Common buyer questions
Is FAT the same as SAT?
No. FAT is performed before shipment under factory test conditions. SAT depends on the buyer's actual site, utilities, mold, material, auxiliaries and operators.
Can a dry-cycle video prove production readiness?
No. A dry cycle can show basic movement and control response, but production readiness also needs mold, resin, process, sample quality and acceptance records.
Should open items block shipment automatically?
Not always. Some items may belong to SAT or buyer-side scope, but every open item should be written with owner, risk, next action and acceptance boundary before shipment release.
Sources and references used for this guide
This guide supports early project planning. Final machine selection and commercial configuration must be confirmed from the actual part, mold, material, factory utilities and production target.