What downstream scope should be written before requesting a turnkey injection molding cell quotation?
Define part removal, conveyor path, cooling time, sorting, inspection, counting, reject handling, packing format, labels, operator responsibility and safety boundary before quotation. Keep selected GEERPOWER cell layout, conveyor model, output, labor saving, price, delivery and FAT/SAT result as NEEDS_EVIDENCE until documented for the exact project.
Decision checklist
- Define finished-part flow before asking for turnkey pricing.
- Decide whether packing is manual-assisted, semi-automatic, automated or excluded.
- State whether parts need cooling, counting, inspection or cavity separation before packing.
- Write where guarding ends and where buyer-side operator responsibility begins.
Turnkey scope continues after demolding
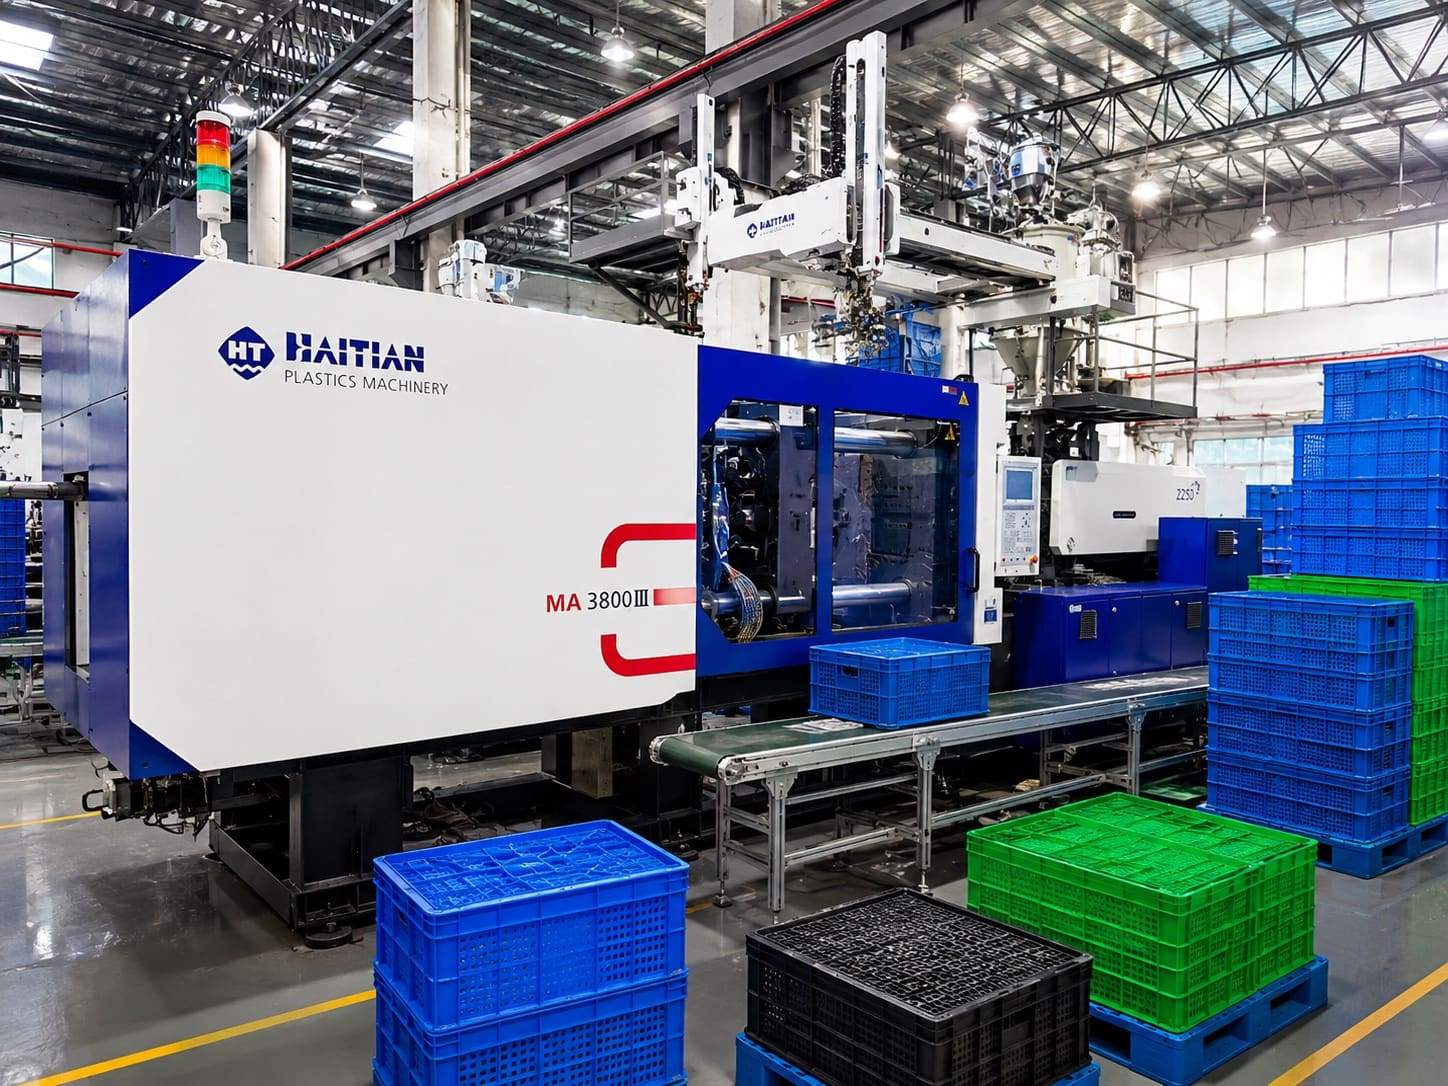
A turnkey injection molding cell is not complete when the molding machine and robot are named. Buyers also need to define what happens after the molded part leaves the mold: conveyor, chute, cooling, sorting, counting, inspection, binning, packing table, cartons, labels, scrap route and operator responsibility.
If this downstream scope is vague, the quotation can hide disputes about layout, labor, guarding, output and acceptance. GEERPOWER should review the downstream plan with the same discipline used for the machine, mold and robot.
A conveyor is not just a belt. It is part of the production flow, quality boundary and labor plan.
Write the downstream table before layout approval
The buyer should provide the finished-part size, weight, temperature sensitivity, cosmetic requirements, cooling need, inspection method, packing format, labor plan and available floor space. GEERPOWER can then separate included equipment from buyer-side work.
A written table prevents one party from assuming automatic packing while the other quoted only a take-out conveyor. It also clarifies whether rejects, runners, samples and mixed cavities follow the same path or need separation.
- Part removal: drop, picker, robot or manual removal and the part-damage risk.
- Conveyor path: length, height, incline, material contact, discharge point and guard boundary.
- Cooling and buffering: air time, part deformation risk, accumulation rule and restart flow.
- Sorting and inspection: OK/NG rule, cavity separation, visual check, weighing or code reading.
- Packing scope: bag, carton, pallet, count, label, operator role and buyer-supplied consumables.
Keep output and labor claims evidence-gated
WITTMANN's auxiliary-equipment pages show how plastics cells can involve material handling, temperature control, robots, conveyors and service support. EUROMAP recommendations cover interfaces between injection molding machines, handling devices and peripheral equipment. These references support scope planning, but not the output of a specific GEERPOWER cell.
Final acceptance depends on the buyer's part, mold, cycle, resin, inspection rule, packing method, operators and factory layout. Labor saving, packing output and quality yield should remain open until the exact cell and FAT/SAT method are documented.
Common buyer questions
Is a conveyor automatically included in a turnkey injection molding cell?
No. It should be written into the scope with length, discharge point, part contact, guarding, reject handling and acceptance requirements.
Should packing be part of the machine quotation?
Only if the buyer wants it included. Packing format, count, labeling, cartons, pallets, consumables and labor responsibility should be defined before pricing.
Can GEERPOWER claim output from the conveyor scope alone?
No. Output depends on the machine, mold, resin, cycle, part handling, packing method, operators and acceptance conditions.
Sources and references used for this guide
This guide supports early project planning. Final machine selection and commercial configuration must be confirmed from the actual part, mold, material, factory utilities and production target.