On this page
What should a buyer agree before accepting the pull-out and rotational torque performance of a molded-in threaded insert?
Define the actual plastic assembly, insert and mating hardware, then agree separate axial pull-out and rotational torque assessment methods. Record fixtures, loading conditions, sample identity, required limits and failure classifications before testing. Review assembly-specific evidence rather than transferring a catalog value to a different resin or geometry. Test availability and final acceptance requirements must be confirmed for the project.
Decision checklist
- Identify the insert, resin, molded component and mating hardware by revision and lot.
- Separate axial retention, resistance to insert rotation and the finished joint's service requirement.
- Agree the fixture, loading arrangement, failure definition and application-specific limits.
- Preserve individual sample results and failure photographs instead of only an average.
- Record who approves deviations and which changes require renewed review.
Buy an accepted joint, not an isolated catalog number
An industrial enclosure may use threaded inserts to support repeated fastening. A supplier can identify the insert and show a clean thread, yet the buyer still needs evidence that the assembled connection meets the product requirement. This is an illustrative application, not an existing GEERPOWER production case.
SPIROL's performance white paper explains that insert performance depends on the plastic, component geometry, installation quality and mating arrangement, as well as the insert. It also cautions against treating catalog performance as a benchmark for a different application. The procurement implication is straightforward: state the actual joint and acceptance question before asking for a test result.
This guide addresses evidence for molded plastic assemblies. It does not select an insert size, prescribe a load limit or certify an installation process. Safety-critical joints require the responsible product engineer to define the applicable validation requirements. Testing and machine operation belong with qualified personnel using an approved procedure.
Distinguish the questions before comparing test reports
Pull-out and rotational torque describe different challenges to the insert's retention. Neither term should become a catch-all label for the entire assembled product. The buyer must also explain the joint's intended fastening and service conditions so the test team can identify which assessment is relevant.
The original comparison below helps purchasing, quality and engineering teams request the same evidence. It is not a replacement for a validated test method. Complete the project-specific fields before ordering samples; leaving them blank until a result is available invites selective interpretation.
| Question | Evidence to define | Do not assume |
|---|---|---|
| Axial retention | Approved pulling arrangement, component support, loading condition and axial failure rule | A torque result establishes pull-out resistance. |
| Resistance to rotation | Approved torque arrangement, engagement, fixture and insert-rotation criterion | The tightening torque and the rotation test are interchangeable. |
| Assembly suitability | Mating component, screw, engagement, use conditions and required product checks | An isolated retention result qualifies the complete product. |
| Production consistency | Cavity and lot identities, agreed sampling and change records | A single development sample represents future production. |
| Commercial release | Signed acceptance criteria, complete report and authorized concessions | A supplier's internal pass label closes every purchase-order requirement. |
Freeze the specimen and fixture definition
Record the component drawing and revision, resin grade, filler specification when relevant, insert reference and insert lot. Identify whether the insert was placed during molding or installed afterward. Do not pool results from different routes without an explicit engineering reason and a clear label.
Ask the test owner for a diagram or photograph of the specimen support and loading direction, together with the method identifier and controlled settings. Document the mating hardware and engagement used in the test. A number without that context can be impossible to compare with the receiving plant's report.
Agree the specimen state before comparison. If the product specification requires particular storage, conditioning, temperature or service exposure, identify those requirements and the evidence expected. This article sets no universal conditioning period or environmental limit. The product owner and responsible test provider must define the relevant conditions.
Preserve any difference between a development coupon, a cut section and the complete molded component. Each can answer a useful question, but they are not automatically equivalent specimens. State which submission supports the final product decision and which evidence remains developmental.
Keep failure evidence attached to the measured value
Request individual sample identifiers, recorded values, relevant observations and photographs of the failure or stopping condition. Ask the report author to distinguish insert movement, plastic damage, thread damage, hardware failure and a test interrupted before the agreed endpoint. These categories are a buyer's documentation checklist, not predefined pass or fail decisions.
If a fixture or mating fastener limits the observation, the report should describe that limit. It should not silently relabel the event as the insert's ultimate capacity. Where the result cannot answer the agreed acceptance question, assign the next action and retain the original record.
For multiple cavities or production lots, keep those identities visible. Agree the sampling basis, individual acceptance rule and treatment of anomalies with the responsible quality team. Do not choose a sample count or average away a weak observation after seeing the results. Any concession should identify the affected scope and the person authorized to accept it.
Connect insert placement and molding evidence to the review
SPIROL describes molded-in inserts as being positioned in the mold before injection and notes the importance of plastic engagement with the insert's retention features. Its technical guidance supports reviewing the placement and molded interface; it does not prove that a particular proposed assembly meets its load requirement.
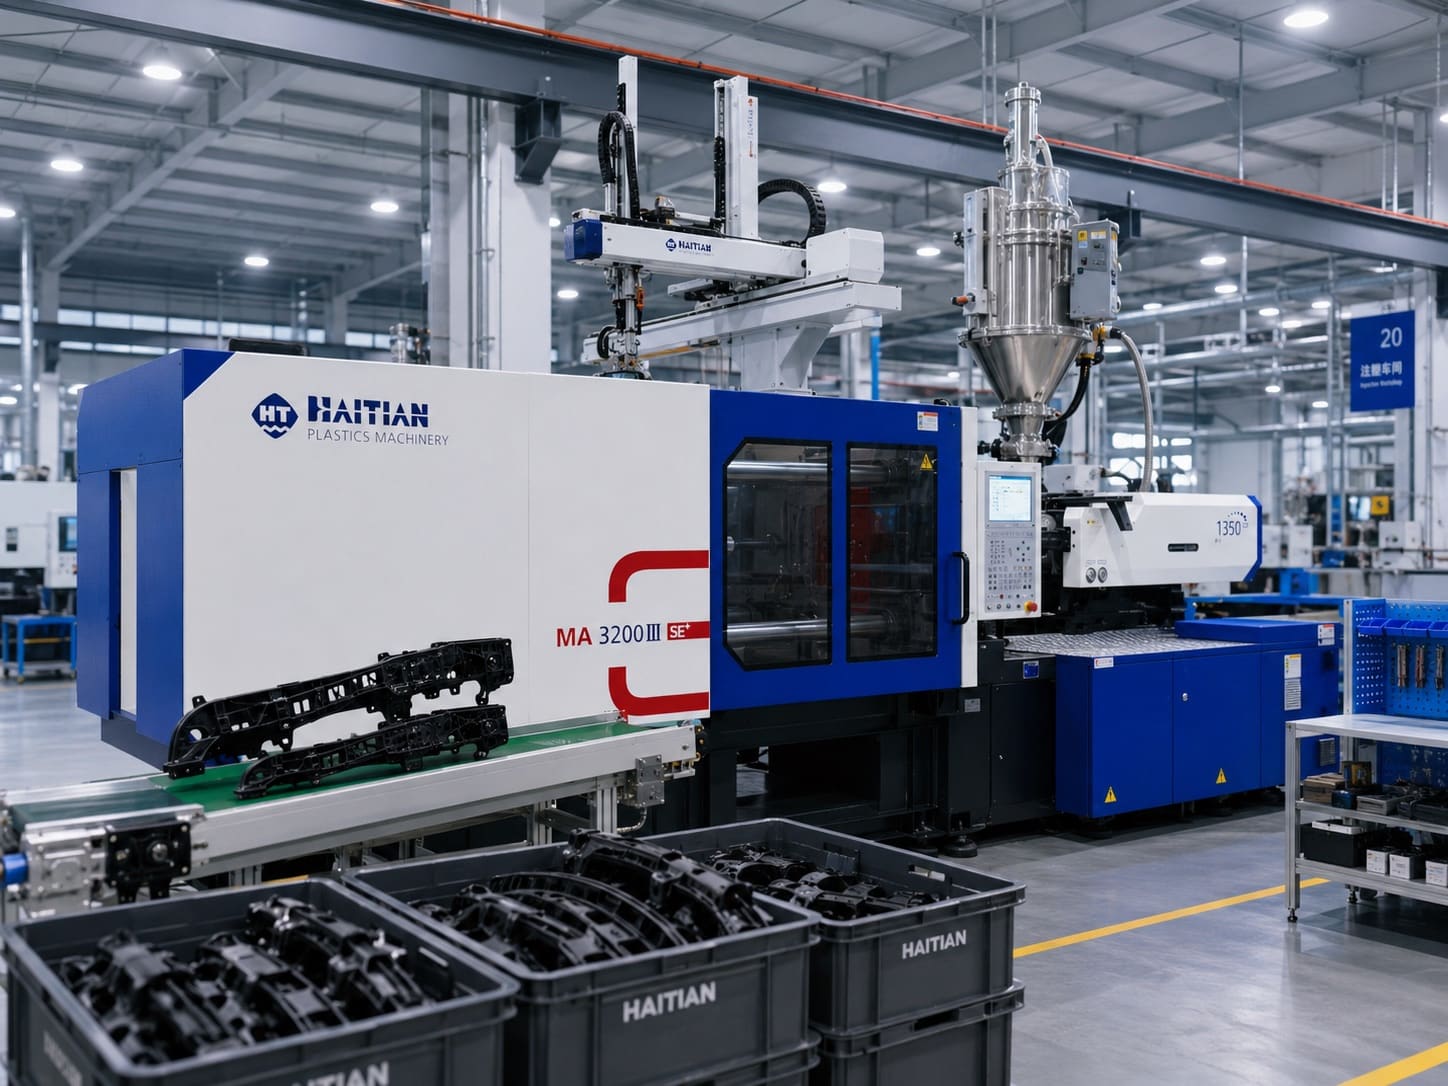
For the project brief, ask how insert identity, presence, orientation where relevant and placement will be checked. Record the responsibility for these checks whether loading is manual or automated. If a camera, robot or other monitoring station is proposed, define what it detects and how a missing or incorrect insert is handled. Do not assume that a vision pass also establishes retention strength.
Include the agreed evidence in the mold and cell handover: approved insert reference, relevant mold and part revisions, placement checks, trial observations, test reports and open actions. If the material, insert, joint geometry or process route later changes, the product owner should determine the revalidation scope before treating previous approval as transferable.
Make supplier quotations comparable
A useful RFQ separates tooling, insert supply, molding, placement or handling equipment, inspection and any external testing. State who supplies the mating hardware, who approves the method and who pays for repeat testing after a design change. A supplier should identify what is included and what requires a separate technical or commercial review.
Send Geerpower Holdings Limited the assembly drawing, insert reference, resin, mating hardware details, target quantities and the retention question you need resolved. Add the required loads and method if your engineering team has already defined them; otherwise identify those fields as open rather than guessing.
Actual insert performance, test-provider identity, testing availability, automation configuration, certifications, sample results, price and delivery remain NEEDS_EVIDENCE until confirmed for the specific project. No owned testing facility, guaranteed joint strength or completed customer application is claimed by this guide.
Common buyer questions
Can a catalog pull-out value be used as our acceptance limit?
Not without establishing that it is appropriate to the actual assembly and approved method. Catalog test materials and configurations may differ from your product.
Does a successful torque test prove pull-out strength?
No. Define the axial and rotational questions separately, then review the finished joint against the product's own requirements.
Can vision inspection replace retention testing?
A vision station can assess only the features and conditions covered by its agreed detection scope. An insert-presence check does not by itself establish mechanical retention.
What should we send before requesting a quotation?
Send the assembly drawing and revision, resin, insert and fastener references, quantities, intended service conditions and any existing test method or limits. Identify unresolved acceptance fields clearly.
Sources and references used for this guide
This guide supports early project planning. Final machine selection and commercial configuration must be confirmed from the actual part, mold, material, factory utilities and production target.